Employment Application Apply
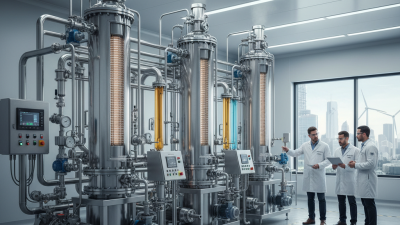
Choosing the best wiped film evaporator in 2026 requires more than comparing heating areas, motor speeds, or supplier promises. The right machine must match the feed, target temperature, viscosity, residence time, and product sensitivity. A sticky polymer solution may need different rotor clearance than a heat-sensitive botanical extract. A solvent-rich stream may demand stronger vapor handling and tighter sealing.
Dr. James R. Fair, a respected separation-process specialist, puts the principle clearly: “The best evaporator is the one that matches the feed, not the one with the highest rated capacity.” This advice remains practical. Capacity figures can look impressive on paper, yet poor distribution may leave thick deposits around the wall. That problem wastes energy and complicates cleaning.
A reliable evaluation should examine real operating conditions. Ask for pilot-test data using your material. Check evaporation rate, outlet quality, fouling behavior, and vacuum stability. Review rotor design, wiped-film thickness, heating uniformity, and maintenance access. Supplier experience also matters, especially when the feed changes seasonally or contains unpredictable solids.
There is no perfect machine.
Even experienced engineers can underestimate scale-up risks. Laboratory results may not reflect continuous production, and a small change in viscosity can alter film formation. This guide will compare the key technical, commercial, and service factors behind a confident wiped film evaporator selection. It will also highlight questions that buyers often miss before signing an equipment specification.
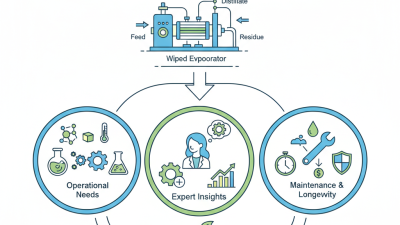
A wiped film evaporator is a thin-film separation device for heat-sensitive, viscous, or difficult-to-distill materials. Its heated cylindrical wall transfers energy while rotating wipers spread liquid into a controlled film. Feed enters near the top and travels downward under gravity and rotor movement. Vapor leaves through a separate outlet, while concentrated liquid reaches the bottom. The film is often only a few millimeters thick. That matters.
Thin films shorten residence time and improve heat transfer, reducing prolonged exposure to high temperatures. A vacuum lowers boiling temperature, which can protect volatile components and reduce thermal stress. In practical trials, operators should watch feed rate, wall temperature, vacuum stability, and rotor speed. A small change in rotor speed can alter film coverage and product quality. Do not rely on catalog capacity alone. Viscosity changes with temperature, and laboratory results may not scale perfectly. This is where judgment matters.
When choosing a unit in 2026, match the evaporation area and construction materials to the actual feed. Request data for viscosity, solids content, boiling range, fouling tendency, and required throughput. Check whether the wiper design handles the product without excessive shear or dead zones. Inspect seals, cleaning access, vacuum connections, temperature controls, and instrumentation. A useful test should measure both recovery and product quality. Unexpected foaming or deposits can expose weaknesses hidden by ideal test conditions. Record those failures. They reveal more than polished performance claims.
Typical feed-viscosity ranges help determine whether a wiped film evaporator can provide effective film renewal, heat transfer, and stable operation.
Wiped film evaporators are commonly considered for feeds ranging from low-viscosity liquids to highly viscous concentrates and polymer-rich materials. The values shown are representative engineering screening ranges in mPa·s; actual limits depend on feed temperature, shear sensitivity, solids content, fouling tendency, rotor design, and required evaporation rate.
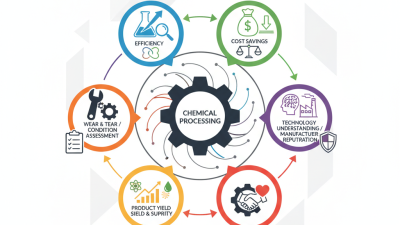
Choosing a wiped film evaporator starts with the feed, not the equipment catalogue. Record viscosity at operating temperature, solids content, volatility, and expected fouling. A thin, heat-renewed film suits heat-sensitive materials when residence time stays short. Ask how the feed behaves after concentration. Some liquids become surprisingly stubborn.
Define the target evaporation rate, pressure range, and allowable product temperature before comparing designs. Vacuum performance matters when boiling points rise or oxidation becomes a concern. Measure vapor load carefully; an undersized condenser can destabilize the entire system. Rotor speed, scraper clearance, and jacket duty should match the real viscosity curve. Do not rely on one laboratory number. Pilot trials reveal wall wetting, foaming, entrainment, and deposits that spreadsheets often miss. A first estimate can be wrong.
Materials of construction should tolerate the feed, cleaning chemistry, and repeated thermal cycling. Check seals, bearings, heating zones, instrumentation, and access for inspection. Operators need stable control of pressure, feed rate, rotor speed, and temperature. Ask for documented test data, maintenance intervals, and clear acceptance criteria. In plant evaluations, easy cleaning is often valued too late. That mistake costs time. The selection should leave room for process variation, because real feed conditions rarely remain perfectly consistent.
How to Choose the Best Wiped Film Evaporator in 2026?
Comparing wiped film evaporator designs starts with the process, not the brochure. My first comparison was too simple. I focused on capacity and overlooked residence time. Short residence time protects heat-sensitive materials from unnecessary thermal exposure. A vertical design often supports efficient gravity flow and continuous operation. A horizontal design may suit limited headroom or unusual feed behavior. Check rotor speed control, scraper geometry, heating-zone length, and vapor outlet size. These details affect film thickness, throughput, and cleaning effort.
Material selection deserves equal attention. Stainless steel can provide practical corrosion resistance for many processes. Hastelloy-type alloys may be considered when chloride exposure or aggressive chemistry is expected. Glass-lined surfaces offer strong chemical resistance, but impact damage requires careful handling. Surface finish matters. Rough welds can hold residue and complicate sanitation. Ask for material certificates, weld inspection records, and documented surface measurements. A reliable supplier should explain test methods, not just provide attractive numbers.
Look closely at seals, bearings, and thermal expansion allowances. Mechanical seals need compatibility with temperature, pressure, and the processed fluid. I once underestimated maintenance access, and a small inspection task became a long shutdown. That mistake still influences my evaluations. Request trial data using a representative feed, including viscosity and solids content. Compare actual evaporation rate, product temperature, energy use, and residual hold-up. Published performance can be useful, but plant conditions are rarely perfect. Leave room for uncertainty.
How to Choose the Best Wiped Film Evaporator in 2026?
What Operating Features Improve Efficiency, Control, and Product Quality?
A suitable wiped film evaporator should match the feed, target temperature, and required residence time. A variable-speed rotor helps maintain a stable, thin liquid film across changing viscosities. This improves heat transfer without exposing the product to excessive thermal stress. Short residence time matters. It can protect color, aroma, and sensitive compounds during evaporation. Look for independent control of jacket temperature, vacuum pressure, feed rate, and rotor speed. These controls let operators adjust one condition without disturbing the others. That level of control supports repeatable production. It also makes troubleshooting less speculative.
Product quality depends on measurement, not attractive specifications. Temperature sensors should monitor both the heating surface and product outlet. Pressure transmitters should respond quickly to vacuum changes. Torque monitoring can reveal rising viscosity, poor wetting, or an overloaded rotor. Useful alarms prevent small deviations from becoming expensive batches. Hygienic construction, drainable surfaces, and practical cleaning access reduce contamination risks between campaigns. In plant trials, high advertised throughput can mislead when the feed contains solids or fluctuating moisture. A smaller system may perform better under real conditions. Review actual test data, cleaning time, energy use, and product recovery before choosing. Some decisions still require compromise.Winvalid
| Operating Feature | Practical Selection Data | Efficiency Benefit | Control and Product-Quality Benefit | What to Verify Before Purchase |
|---|---|---|---|---|
| Operating Pressure and Vacuum Stability | Specify the required pressure range, commonly from approximately 1 to 100 mbar absolute for vacuum evaporation applications. The final value depends on the product boiling point and thermal sensitivity. | Lower pressure reduces the boiling temperature and can lower the required heating-medium temperature. | Improves protection of heat-sensitive materials and helps maintain a consistent evaporation endpoint. | Check vacuum-pump capacity, condenser sizing, air-leak testing, pressure-control response, and pressure stability at maximum vapor load. |
| Short and Controlled Residence Time | Choose a vertical falling-film or wiped-film configuration when product exposure must be limited to seconds or a few minutes, depending on viscosity, feed rate, and equipment geometry. | Short exposure reduces unnecessary heating and supports continuous processing. | Limits thermal degradation, discoloration, oxidation, polymerization, and loss of volatile components. | Request residence-time data based on the actual feed properties, not only an empty-equipment rating. |
| Wiper or Rotor Speed Control | Use variable-speed control; many industrial designs operate within a broad range of roughly 100–600 rpm, while the suitable setting depends on rotor diameter, viscosity, and film thickness. | Allows the operator to balance heat transfer, throughput, and film renewal. | More uniform wetting can reduce hot spots, fouling, local over-concentration, and product-quality variation. | Confirm speed range, torque margin, overload protection, vibration monitoring, and whether the rotor is suitable for the expected viscosity. |
| Adjustable Feed Rate | Select a metering system capable of stable low-flow operation and turndown. The required range should be based on the process capacity and target evaporation rate. | Prevents overloading of the heated surface and improves energy use at different production rates. | Supports consistent concentration, reduces dry spots, and makes start-up and shutdown easier to control. | Evaluate pump compatibility with viscosity, solids content, shear sensitivity, and minimum stable flow. |
| High Heat-Transfer Surface Utilization | Specify the effective heated area, heat-transfer coefficient, heating-medium temperature, and allowable wall-temperature difference. Actual performance should be confirmed with product-specific trials. | Efficient surface utilization can increase evaporation capacity without excessive heating temperature. | Uniform wall temperature reduces localized overheating and helps protect sensitive compounds. | Ask for heat-transfer data using a feed with comparable viscosity, solids concentration, boiling point, and fouling tendency. |
| Independent Heating-Zone Control | Use multiple temperature zones when the product changes significantly in viscosity or concentration during evaporation. | Distributes the thermal load more effectively and avoids over-heating areas that require less heat. | Provides better control of film behavior, final concentration, color, and thermal history. | Check the number of zones, temperature sensors, control-loop response, and minimum controllable temperature difference. |
| Efficient Vapor-Liquid Separation | Include an appropriately sized vapor outlet, demister or entrainment separator, and condenser system based on vapor rate and composition. | Reduces liquid carryover and helps maintain stable vacuum operation. | Improves product recovery, protects downstream vacuum equipment, and reduces contamination of condensate. | Verify allowable vapor velocity, pressure drop, demister cleanability, condensate handling, and solvent compatibility. |
| Fouling and Residue Management | Favor rotor designs that continuously renew the film and maintain mechanical contact with the heated wall. The required cleaning interval must be established through testing. | Maintains heat-transfer performance and reduces unplanned downtime. | Reduces contamination from burnt or aged residue and improves batch-to-batch consistency. | Review clean-in-place capability, drainability, inspection access, surface finish, and compatibility with the proposed cleaning chemicals. |
| Material of Construction and Surface Finish | Common wetted materials include stainless steels such as 316L; higher-alloy materials or special coatings may be required for corrosive feeds. Surface finish should be selected for hygiene and fouling control. | Durable, corrosion-resistant surfaces reduce maintenance and product loss caused by equipment degradation. | Minimizes metal contamination, adsorption, corrosion products, and cleaning-related quality risks. | Confirm corrosion compatibility, weld quality, surface roughness, gasket materials, and applicable hygienic or sanitary requirements. |
| Mechanical Seal and Vacuum Integrity | Select seals rated for the operating temperature, pressure, shaft speed, solvent exposure, and required service life. | Reduces vacuum loss, air ingress, solvent loss, and stoppages caused by seal failure. | Helps prevent oxidation, moisture ingress, and contamination of the processed material. | Check seal arrangement, purge requirements, leakage detection, replacement procedure, and availability of compatible seal materials. |
| Instrumentation and Automated Control | At minimum, monitor feed rate, rotor speed, heating temperature, product temperature, absolute pressure, condenser temperature, and motor load. | Enables repeatable operation and faster response to changes in feed or vapor load. | Improves endpoint control and supports traceability of critical process conditions. | Verify sensor accuracy, calibration intervals, alarm limits, data logging, recipe control, and integration with the plant control system. |
| Energy Integration and Heat Recovery | Assess vapor recompression, preheating with condensate, feed heat recovery, and multi-effect operation where the process scale justifies it. | Can reduce steam or electrical demand per unit of evaporated water or solvent. | Lower heating demand can reduce thermal stress when operating temperatures are correspondingly reduced. | Compare total energy consumption, condenser duty, utility temperatures, operating complexity, and payback under the expected production schedule. |
| Solids, Viscosity, and Particle-Handling Capability | Define the feed viscosity at operating temperature, solids content, particle size, crystallization tendency, and required final concentration. Wiped-film units are often selected for viscous or concentrated products, but limits are equipment-specific. | Correct sizing prevents excessive motor load, poor wetting, blocked outlets, and loss of capacity. | Maintains a stable film and reduces shear, plugging, and concentration variation. | Require pilot testing with representative material, including start-up, steady state, upset conditions, and shutdown behavior. |
| Product Recovery and Bottoms Discharge | Choose a discharge design that matches the final viscosity, solids level, crystallization risk, and required residual solvent or moisture content. | Reduces hold-up and product losses at the outlet. | Improves consistency of the concentrated product and reduces degradation during discharge. | Verify discharge temperature, outlet geometry, torque requirements, drainability, and the ability to prevent back-mixing. |
| Pilot Testing and Scale-Up Basis | Use representative feed testing to establish evaporation rate, heat duty, residence time, pressure, rotor speed, fouling rate, and final product quality. | Reduces the risk of selecting excessive or insufficient heat-transfer area. | Confirms whether color, potency, viscosity, purity, aroma, or residual-solvent specifications are maintained. | Insist on a documented scale-up method and test results obtained under conditions close to the intended production process. |
Evaluate total cost, not only the equipment quotation.
A reliable comparison includes purchase price, installation, vacuum power, heating media, cleaning labor, spare rotors, seals, and disposal costs. The U.S. Department of Energy’s 2022 Industrial Decarbonization Roadmap reports that process heating represents about 51% of industrial energy use. Therefore, thermal efficiency deserves serious attention. Ask for utility consumption at your actual feed rate. Laboratory figures can look attractive.
Maintenance is where many projects become expensive.
Request rotor runout limits, seal-life data, inspection intervals, and a written spare-parts list. McKinsey’s 2018 Predictive Maintenance 4.0 report indicates potential maintenance-cost reductions of 10–40% through better condition monitoring. Add vibration checks and temperature trending where practical. Keep it simple. A spreadsheet is never the whole truth. Operators should inspect a pilot unit, hear its drive system, and examine deposits after a realistic trial.
Safety and supplier support require equal weight.
Review pressure protection, vacuum-break procedures, guarding, solvent compatibility, inerting needs, and hazardous-area documentation with qualified engineers. Request a documented HAZOP before commissioning. Supplier support should include factory testing, site acceptance testing, operator training, emergency response times, and local critical spares. Ask for references using comparable viscosity and thermal sensitivity. A low bid with weak service can create long downtime. I would also reserve budget for redesign; feed behavior is often less predictable than the sales specification.