7 Tips for Choosing the Right Wide Film Evaporator

Selecting the right wide film evaporator can determine whether a production line runs smoothly or struggles with unstable concentration. The choice affects heat transfer, residence time, energy use, product quality, and maintenance demands. A unit that looks efficient on paper may perform poorly with a viscous, heat-sensitive, or foaming feed.

Real process experience matters here. Operators often notice issues before spreadsheets do. A film may break unevenly. Deposits may appear near the discharge zone. Vacuum fluctuations can quietly reduce capacity. Small details matter.

This guide presents seven practical tips for evaluating equipment with greater confidence. It considers feed viscosity, evaporation rate, thermal sensitivity, rotor design, surface materials, cleaning access, and supplier support. These factors should be checked against pilot data, operating records, and realistic production conditions.

Do not trust capacity figures alone.

A reliable decision also requires questions about commissioning, spare parts, control systems, and long-term service. Experienced engineers can compare heat-transfer areas, residence times, and operating temperatures without ignoring the product’s behavior. Still, no calculation is perfect. Feed composition may change between batches, and laboratory results may not predict every factory challenge.

That uncertainty deserves attention. A careful selection process combines technical evidence with practical observation. It also leaves room for adjustment after installation. The following tips will help buyers assess whether a wide film evaporator truly matches their process, facility, and future production goals.
7 Tips for Choosing the Right Wide Film Evaporator

Understanding Wide Film Evaporator Design and Operating Principles

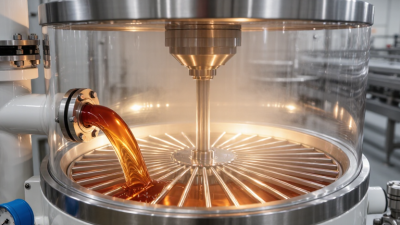
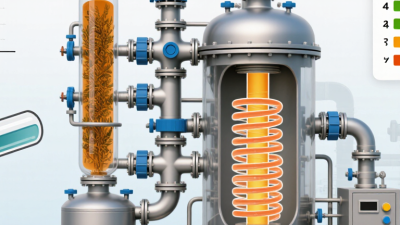
A wide film evaporator spreads liquid across a broad heated surface as a thin, moving layer. Its design controls heat transfer, residence time, and product exposure. A distributor must wet the surface evenly. Dry patches can create hot spots, scaling, and uneven concentration.

The feed rate, viscosity, and boiling temperature must match the rotor and heating area. A slower rotor may increase residence time, but it can also encourage deposits. A faster rotor improves renewal of the film, although excessive speed may raise power use and entrainment. Keep it simple. Measure the outlet temperature, pressure, motor load, and product concentration during each trial.

Good vacuum control lowers the boiling point and protects heat-sensitive materials. The condenser must handle the vapor load without causing pressure swings. Inspect seals, scraper clearance, and feed nozzles regularly. Small leaks matter. In field operation, I have seen a partially blocked distributor cause unstable output within minutes. Cleaning solved the symptom, but the deeper issue was poor upstream filtration. That lesson is easy to overlook. Design reviews should also consider cleanability, access, drainage, and future maintenance time. A wide evaporator may offer high capacity, yet capacity alone does not prove good performance. Test the actual feed, because laboratory fluid behavior rarely matches production conditions perfectly.

Assessing Feed Properties and Processing Requirements

Choosing a wide film evaporator starts with the feed, not the equipment brochure. Measure viscosity at operating temperature, suspended solids, moisture, and dissolved salts. A feed that pours easily at 25°C may move slowly under vacuum. That difference affects film coverage and heat transfer.

Heat sensitivity deserves close attention. Record the target concentration, allowable product temperature, and maximum residence time. Foaming feeds may need gentle vapor removal and suitable demisting capacity. Sticky or sugar-rich liquids can form deposits near the heating surface. Small particles can also disturb distribution across a wide rotor. Real data matters more than assumptions.

Run a pilot test with representative material. Check throughput, outlet moisture, product color, viscosity, and cleaning time. Watch the feed pattern through inspection points. Uneven wetting is a warning sign. Operators should also compare performance during start-up and after several hours. A clean trial can mislead. Fouling often appears later, when the surface temperature rises and the feed becomes concentrated. This is where the design may need revision, not optimism. Consider upstream filtration, feed preheating, vacuum stability, and the required operating range. A practical specification should state these values clearly, including variations between batches. Even experienced teams miss one detail: seasonal changes in raw material can alter viscosity enough to reduce capacity.

7 Tips for Choosing the Right Wide Film Evaporator - Assessing Feed Properties and Processing Requirements

Tip Feed or Process Dimension Typical Data to Assess Why It Matters Selection Guidance
1 Confirm thermal sensitivity Maximum allowable product temperature, degradation onset, color change, oxidation sensitivity, and target residence time. Thin-film equipment spreads the feed into a relatively short, continuously renewed film, reducing heat-transfer resistance and exposure time compared with many batch systems. For heat-sensitive materials, prioritize vacuum operation, rapid film renewal, accurate temperature control, and the shortest practical residence time. A product limit below approximately 100 °C generally requires careful thermal design and vacuum selection.
2 Measure viscosity across temperature Viscosity at feed temperature, evaporation temperature, and concentration endpoint; include shear sensitivity and yield stress where applicable. Viscosity affects pumping, distributor performance, film uniformity, rotor load, heat transfer, and the risk of stagnant regions. Low- to medium-viscosity feeds are usually easier to distribute. For concentrated feeds above roughly 1,000 mPa·s, verify torque, discharge design, feed preheating, and the manufacturer’s maximum operating viscosity using actual rheology data.
3 Check solids, particles, and suspended matter Total dissolved and suspended solids, particle-size distribution, abrasive content, and the largest particle that may enter the system. Solids can increase viscosity, obstruct feed distributors, accelerate wear, and promote deposits on heated surfaces. Remove oversized particles upstream where possible. For abrasive or particulate feeds, consider larger clearances, wear-resistant wetted parts, cleanable internals, and a bottom outlet designed to prevent bridging.
4 Evaluate fouling and deposition tendency Historical cleaning frequency, maximum concentration factor, crystallization point, polymerization risk, and deposit composition. Fouling lowers the overall heat-transfer coefficient, increases pressure drop, and can create hot spots or unstable operation. Select continuous wiping or scraping action when deposit control is important. Specify clean-in-place or manual-cleaning access, removable internals, and a validated cleaning procedure for the actual residue.
5 Define evaporation load and boiling behavior Feed rate, solvent type, vaporization rate, boiling-point range, dissolved-gas content, foaming tendency, and required outlet concentration. The evaporation duty determines heat-transfer area, vapor capacity, condenser size, entrainment control, and operating stability. Calculate duty from mass balance and enthalpy data rather than feed flow alone. Include latent heat, sensible heat, heat losses, and a practical design margin; confirm vapor disengagement capacity for foaming feeds.
6 Match vacuum and pressure requirements Target absolute pressure, boiling temperature, non-condensable gas load, vacuum-system capacity, and allowable air leakage. Lower absolute pressure reduces boiling temperature, but it also increases vapor volume and may increase entrainment or condenser demand. Size the vapor line, demister, condenser, and vacuum system together. For water-based feeds, operation under approximately 50 kPa absolute can materially lower boiling temperature, subject to the product’s vapor-pressure and heat-transfer requirements.
7 Verify materials, hygiene, and maintainability Product chemistry, chloride or acid content, corrosion rate, required surface finish, hygienic design, inspection access, and cleaning validation. Material compatibility and cleanability affect equipment life, product purity, downtime, and regulatory compliance. Select wetted materials from corrosion-test data rather than concentration alone. For hygienic processes, specify drainable geometry, suitable surface finish, sanitary connections, validated cleaning, and documented elastomer compatibility.

Note: The operating ranges are general engineering reference points. Final evaporator sizing and configuration should be confirmed through mass and energy balances, laboratory testing, pilot trials, and product-specific materials-compatibility evaluation.

Comparing Capacity, Heat Transfer, and Energy Efficiency

Choosing the Right Wide Film Evaporator: Comparing Capacity, Heat Transfer, and Energy Efficiency

Capacity should match the real process, not the brochure maximum. Record feed rate, solids content, viscosity, and target concentration during normal and peak operation. The U.S. Department of Energy’s Manufacturing Energy and Carbon Footprints report identifies process heating as roughly 51% of manufacturing energy use. That makes evaporator sizing an operating-cost decision, not merely a production decision. A larger unit may reduce residence time, but it can also waste steam when lightly loaded.

Heat transfer depends on film thickness, surface wetting, temperature difference, and feed distribution. In plant trials, watch the product leaving the distributor. Dry streaks, dark deposits, or unstable flow often reveal poor wetting before laboratory tests do. The International Energy Agency reported that industry remains one of the largest global energy-consuming sectors in its Energy Efficiency 2023 analysis. Therefore, compare evaporation duty per kilogram of water removed, not only hourly throughput. A lower heating temperature may protect sensitive materials, but it can require a larger heat-transfer area.

Energy recovery deserves careful measurement. Check condensate temperature, vapor reuse potential, vacuum-system demand, and cleaning frequency. The U.S. DOE Industrial Technologies Program recommends using measured utility data for process-heating evaluations. Good advice, though plant data is rarely perfect. Measure twice. A pilot test should run at different feed rates and viscosities, while operators record power, steam, fouling, and product quality. A promising result at steady laboratory conditions may change after twelve hours of continuous operation.

Selecting Materials, Configuration, and Equipment Features

Choosing the right wide film evaporator starts with the liquid, not the machine. Confirm viscosity, solids, acidity, chloride level, and heat sensitivity from real production samples. Material selection is critical. Stainless steel may suit mild service, while demanding fluids need stronger corrosion resistance and carefully selected seals. Ask for compatibility data at operating temperature, not room temperature. I have seen a seemingly suitable alloy fail around a gasket after repeated thermal cycles. Small details matter.

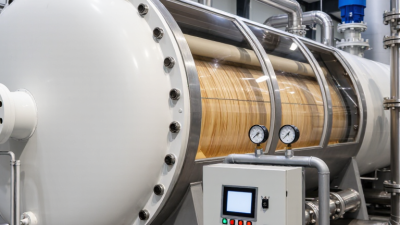
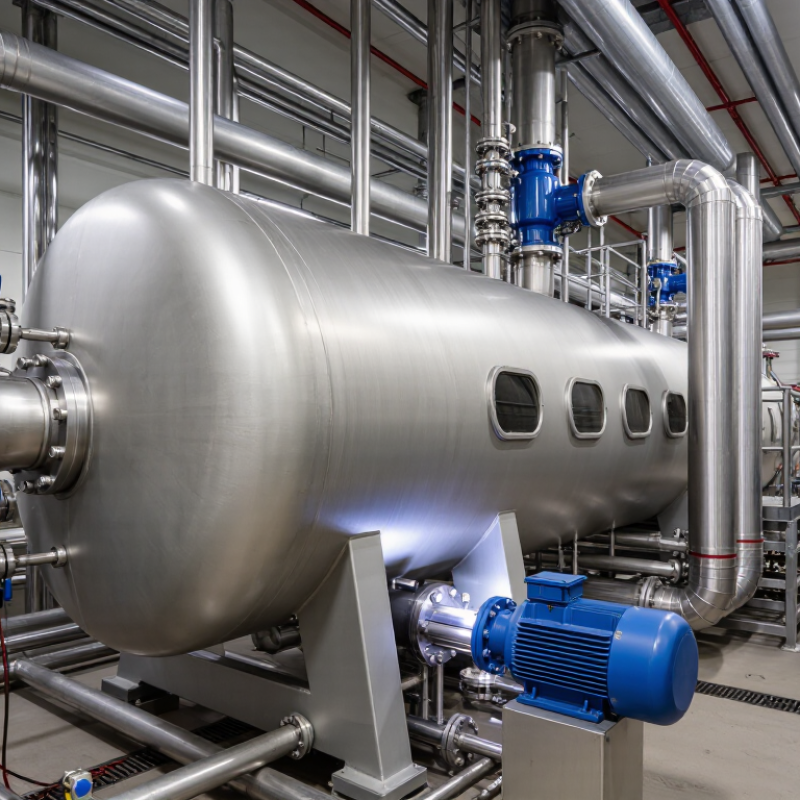
Configuration should match the process. A vertical or horizontal arrangement affects residence time, drainage, and installation height. Select a rotor that spreads liquid into a stable, thin film without excessive shear. Feed distribution deserves close inspection; dry sections can cause fouling and uneven evaporation. Choose single-pass operation for sensitive products when possible, but verify its capacity under peak load. Laboratory results can mislead if the feed is too clean.

Equipment features should support control and maintenance. Look for accurate temperature and vacuum sensors, adjustable heating zones, accessible seals, and sight ports where practical. Smooth internal surfaces simplify cleaning. A robust condenser and correctly sized vacuum system protect evaporation stability. Leave room for inspection. It is often forgotten. Do not judge efficiency from one data point; compare energy use, product quality, cleaning time, and downtime. The best selection is not always the most powerful one. Sometimes, a simpler configuration performs more reliably, though this conclusion should be tested again.

Evaluating Maintenance, Safety, and Total Ownership Costs

Choosing a wide film evaporator starts with maintenance access, not brochure capacity. In operating areas, technicians need clear sightlines to the rotor, seals, bearings, and condenser connections. Ask how quickly a trained team can isolate the unit and replace a worn seal. A removable inspection cover can save hours during a planned shutdown. It can also expose poor gasket design. Measure cleanout time with water and a stopwatch. Estimates are often optimistic.

Safety reviews should cover pressure relief, vacuum protection, hot surfaces, process vapors, and control-system interlocks. Verify that alarms remain visible at eye level. Check the emergency stop, grounding, guarding, and access platforms. Request test records and calibration intervals, not only certificates. A wide rotor can develop serious imbalance when deposits build unevenly. Specify vibration monitoring and a documented response limit. Operators should rehearse a shutdown. Paper procedures alone are weak.

Total ownership cost includes energy, cooling water, labor, consumables, downtime, waste handling, training, and spare parts. Compare power per kilogram evaporated under actual feed conditions, including viscosity changes. Ask for performance data from similar duties, not ideal laboratory liquids. Calculate annual seal replacements and planned maintenance hours. Consider local service expertise; a low-cost part becomes expensive after a week of waiting. I would also price lost production during cleaning. That figure is easy to ignore. Do not ignore it. Leave room for uncertainty, because fouling, feed variation, and inexperienced operation can defeat a perfect spreadsheet.